Welcome to our website!
Cold-Applied Pipeline Wrapping Tape for Bends and Elbows: Selection and Application Guide
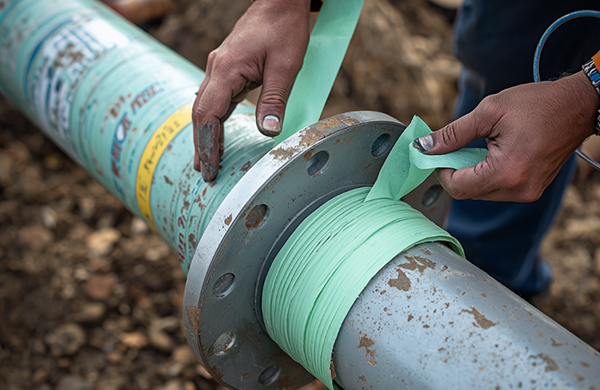
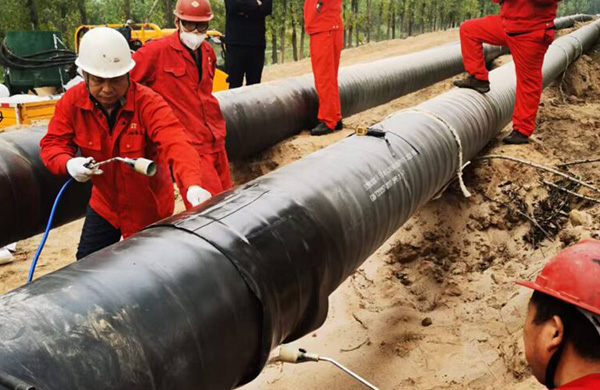
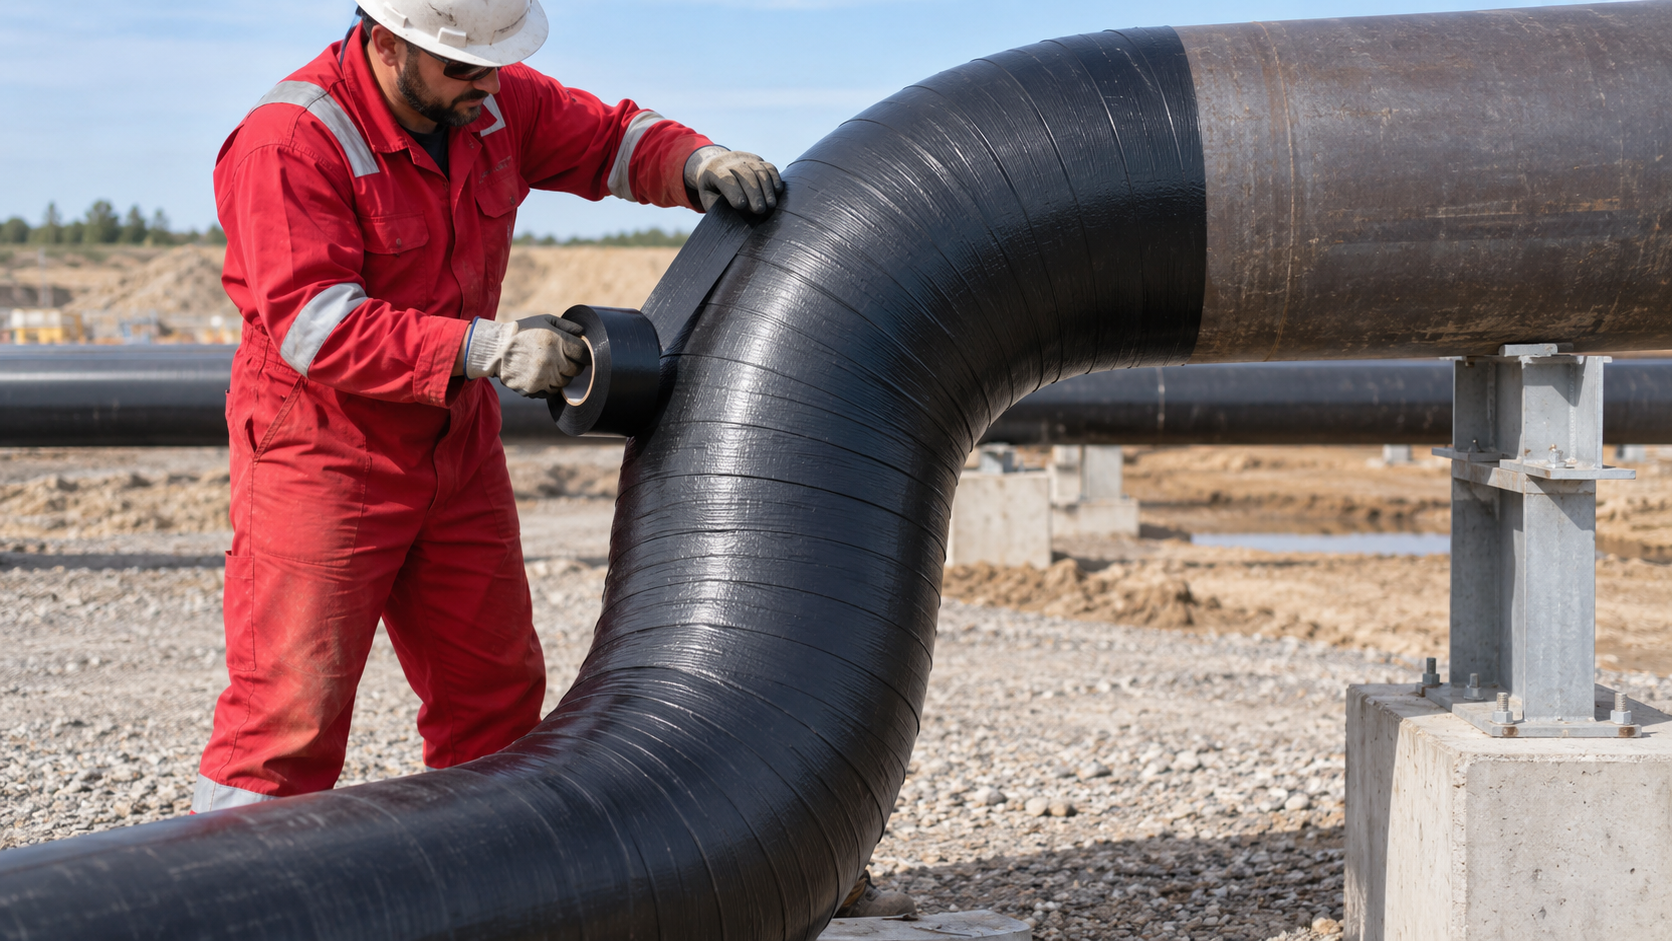
On a straight pipe, the tape follows a regular cylindrical surface, making it relatively easy to control the wrapping angle, tension and overlap. On a bend, however, the inside and outside radii have different circumferences. The tape must continuously adapt to this changing geometry.
If the tape width, flexibility, tension or wrapping method is unsuitable, wrinkles, folds, trapped air, uneven overlap or edge lifting may occur. These defects can weaken the completed coating system and create potential pathways for moisture and electrolytes to reach the steel surface.
Selecting a cold-applied pipeline wrapping tape for bends therefore requires more than confirming the nominal tape thickness. The complete primer, inner wrap tape and outer wrap tape system must be evaluated against the pipe diameter, bend radius, service conditions and project specification.
This guide explains the principal factors that pipeline owners, EPC contractors, coating inspectors and procurement teams should consider when selecting and applying cold-applied tape systems on pipeline bends and elbows.
Why Pipeline Bends Are More Difficult to Wrap
A pipeline bend creates a continuously changing wrapping surface.
As the tape moves around the bend:
It travels a longer distance along the outside radius.
Material tends to accumulate along the inside radius.
The effective overlap may change if the wrapping angle is not controlled.
Excessive tension may stretch or narrow the tape.
Insufficient tension may leave loose areas or trapped air.
Wide tape may resist conforming to a tight bend radius.
Thick or relatively rigid tape may be more difficult to apply without wrinkles.
The problem becomes more significant when the bend radius is small, the pipe diameter is large, or the ambient temperature affects tape flexibility.
These geometric differences mean that a tape system suitable for a long straight section should not automatically be assumed suitable for every bend.
Understand the Complete Coating System
A conventional cold-applied polyethylene tape coating system normally contains three compatible components:
System Component
Primary Function on Pipeline Bends
Primer
Prepares and wets the steel surface and promotes adhesion between the steel and inner wrap tape
Inner wrap tape
Forms the primary corrosion protection and sealing layer
Outer wrap tape
Protects the inner layer against mechanical damage and helps hold the system in position
The three materials should be selected as one complete system.
The primer must be compatible with the adhesive on the inner wrap tape. The inner tape must provide continuous contact and corrosion protection, while the outer tape must protect the inner layer without creating excessive stress, lifting or displacement.
For a broader explanation of these component functions, see:
Inner Wrap Tape, Outer Wrap Tape and Primer: How a Complete Cold-Applied Pipeline Coating System Works
Key Factors in Selecting Wrapping Tape for Pipeline Bends
- Tape Flexibility and Conformability
The tape must be able to follow the bend geometry while maintaining continuous contact with the primed steel or the underlying tape layer.
A suitable tape should conform without:
Forming permanent wrinkles
Bridging over the substrate
Lifting at the edges
Creating air pockets
Losing the specified overlap
Separating between tape layers
Conformability depends on the complete tape construction, including:
Backing material
Backing thickness
Adhesive thickness
Adhesive formulation
Tape width
Application temperature
Applied tension
A tape that feels flexible under normal handling may still behave differently when wrapped under tension around a small-radius bend. For critical applications, actual wrapping trials are more reliable than visual or manual assessment alone.
- Tape Width
Tape width is one of the most important practical considerations for bend application.
Narrower tape can generally follow a changing radius more easily. It may reduce wrinkling and make it easier to maintain consistent contact along both the inside and outside radii.
However, narrower tape also requires:
More wrapping passes
More overlaps
More installation time
More careful quantity calculation
Wider tape can improve productivity on straight pipe sections, but it may be more difficult to conform around a tight bend.
The appropriate width should therefore be selected according to:
Pipe outside diameter
Bend angle
Bend radius
Tape thickness and flexibility
Required overlap
Application method
Installer experience
Project specification
There is no single tape width that is automatically suitable for every bend.
A representative wrapping trial using the actual or equivalent pipe diameter and bend radius is recommended before large-scale application.
- Total Tape Thickness
Total tape thickness is normally the combined thickness of the backing and adhesive:
Total tape thickness = backing thickness + adhesive thickness
However, total thickness alone does not fully describe the function of a wrapping tape.
Two tapes may have the same nominal total thickness but very different constructions.
For example:
An inner wrap tape may use a relatively thicker adhesive layer to improve sealing and contact with the substrate.
An outer wrap tape may use a relatively thicker backing to improve mechanical protection.
A thicker tape may provide a higher coating build, but it may also be more difficult to conform around tight bends. The balance between thickness, flexibility and layer function must therefore be considered.
When comparing products, buyers should request:
Total thickness
Backing thickness
Adhesive thickness
Dimensional tolerances
Applicable test method
Intended use as inner or outer wrap
Required number of layers
Completed system thickness
More information about Jiayu’s tape product range is available on the Cold-Applied Tape product page.
- Backing-to-Adhesive Construction
The backing and adhesive perform different functions.
Inner Wrap Tape
The inner wrap tape is the principal corrosion protection layer. Its adhesive side is applied to the primed steel surface.
Important characteristics include:
Adhesion to primed steel
Adhesion at tape overlaps
Resistance to moisture and electrolyte penetration
Electrical insulation
Conformability
Resistance to edge lifting
Performance at the specified service temperature
Outer Wrap Tape
The outer wrap tape is applied over the inner corrosion protection layer.
Its principal functions include:
Mechanical protection
Resistance to handling damage
Protection during lowering-in and backfilling
Resistance to impact and indentation
Stabilization of the inner coating layer
Protection at overlaps and transition areas
The outer wrap should not be evaluated as if it performs the same function as the inner wrap. Even when both products belong to the same tape series, their backing-to-adhesive constructions may be different.
- Primer Compatibility
Primer is normally an essential part of a conventional polyethylene adhesive tape system.
Its functions may include:
Improving adhesion between steel and inner tape
Wetting the prepared steel surface
Binding small amounts of residual surface dust
Supporting continuous contact at the steel-to-coating interface
Improving the stability of the complete wrapping system
The primer, inner tape and outer tape should preferably be manufactured, recommended or formally approved as a compatible system.
Mixing primers and tapes from unrelated manufacturers without technical confirmation may create risks such as:
Poor adhesion
Solvent entrapment
Blistering
Edge lifting
Interlayer incompatibility
Uncertain temperature performance
Unclear warranty responsibility
Primer coverage, drying condition and application temperature must be confirmed in the manufacturer’s approved technical documentation.
- Application and Operating Temperatures
Application temperature and operating temperature are different technical parameters.
Application temperature refers to the acceptable ambient and substrate temperature range during installation.
Operating temperature refers to the temperature the completed coating system is expected to withstand during service.
Low application temperatures may reduce flexibility and adhesion. High substrate temperatures may affect primer drying and tape handling. Long-term operating temperature may influence adhesive stability, peel strength and mechanical performance.
The proposed system should therefore be evaluated against:
Minimum installation temperature
Maximum installation temperature
Minimum substrate temperature
Maximum pipeline operating temperature
Expected temperature cycling
Storage temperature before installation
The values stated for an individual tape should not automatically be treated as the qualification temperature of the complete coating system.
Tape Width and Bend Geometry
The relationship between tape width and bend geometry is practical rather than purely dimensional.
Bend Condition
General Selection Consideration
Large-radius bend
A wider tape may be practical if it conforms without wrinkles
Small-radius or tight bend
A narrower tape may improve conformability
Large-diameter pipe
Tape width should be balanced against wrapping control and productivity
Complex transition area
Narrower tape or a project-specific wrapping method may be required
Manual field application
Installer control and accessibility become especially important
Repetitive workshop application
A qualified wrapping procedure can improve consistency
These are general considerations rather than fixed design rules.
The final tape width should be confirmed through the manufacturer’s recommendation, project specification and, where necessary, a representative application trial.
Overlap and Wrapping Direction
Overlap directly influences the completed coating thickness, coverage and material consumption.
The application procedure should define:
- Minimum overlap
- Wrapping direction
- Starting point
- Finishing point
- Treatment of the inside radius
- Treatment of the outside radius
- Required application tension
- Number of layers
- Transition onto existing coating
- End-sealing method
The overlap must remain consistent through the bend. If the wrapping angle changes excessively, the inside radius may develop excessive material build-up while the outside radius may have insufficient overlap.
The installer should not compensate for poor conformability by overstretching the tape. Excessive tension can reduce the effective tape width, change the overlap and increase the risk of edge lifting.
Any specific overlap percentage should follow the approved manufacturer’s instructions and the project specification.
Surface Preparation Before Wrapping
Reliable coating performance begins with appropriate surface preparation.
Before primer application, the steel surface should be:
- Free from oil and grease
- Dry and free from moisture
- Free from loose rust and mill scale
- Free from dust, soil and other contaminants
- Free from weld spatter and sharp projections
- Prepared to the cleanliness level specified for the project
Sharp edges, irregular weld profiles and surface projections may damage the tape or prevent complete contact. These areas should be treated before wrapping.
The required surface preparation standard depends on the coating system and project requirements. A general statement such as “clean the pipe” is not sufficient for a controlled installation procedure.
The procedure should identify:
- Required cleanliness grade
- Surface preparation method
- Permitted surface profile
- Dust removal method
- Acceptable surface condition
- Maximum time between preparation, priming and wrapping
General Installation Sequence for Pipeline Bends
The following sequence provides a general overview. The approved manufacturer’s application instructions and project specification must take priority.
Step 1: Confirm the Bend Dimensions
Record:
Pipe outside diameter
Bend angle
Bend radius
Length of the area to be coated
Existing coating type
Required transition length
These dimensions affect tape width, overlap, wrapping passes and total material consumption.
Step 2: Inspect and Prepare the Steel Surface
Remove oil, grease, moisture, dust, loose rust, mill scale, weld spatter and other contaminants.
Complete the specified surface preparation and verify that the surface is dry and suitable for primer application.
Step 3: Apply the Compatible Primer
Mix or stir the primer as instructed by the manufacturer.
Apply a thin and uniform coat without missed areas, excessive accumulation, runs or contamination.
Begin wrapping only after the primer reaches the specified application condition. Tape should not be applied when the primer is excessively wet or fully over-dried unless permitted by the approved procedure.
Step 4: Apply the Inner Wrap Tape
Apply the adhesive side of the inner tape to the primed surface.
During wrapping:
Maintain controlled tension.
Keep the specified overlap.
Press the tape firmly onto the substrate.
Follow the changing geometry of the bend.
Avoid wrinkles and trapped air.
Monitor both the inside and outside radii.
Do not overstretch the tape.
Ensure complete contact at the start and finish points.
Step 5: Apply the Outer Wrap Tape
Apply the compatible outer wrap over the completed inner layer.
Ensure that:
The inner tape is fully covered.
The specified overlap is maintained.
Wrinkles and folds are avoided.
The outer tape does not displace the inner layer.
Start and finish areas are securely completed.
Transition areas are properly protected.
Step 6: Inspect the Completed Coating
The completed coating should be inspected for:
Wrinkles
Folds
Loose edges
Inconsistent overlap
Trapped air
Physical damage
Unprotected areas
Incorrect start or finish details
Coating discontinuities
Separation between layers
Any defect should be repaired using an approved procedure before the pipe is lowered into the trench, backfilled or returned to service.
Common Installation Problems on Pipeline Bends
| Problem | Possible Cause | Recommended Action |
|---|---|---|
| Wrinkles on the inside radius | Tape too wide, excessive material accumulation or incorrect wrapping angle | Review tape width, angle and wrapping technique |
| Insufficient overlap on the outside radius | Wrapping angle not controlled or tape overstretched | Reduce tension and maintain the approved overlap |
| Edge lifting | Poor surface preparation, incorrect primer condition or excessive tape stress | Verify surface condition, primer application and tape tension |
| Trapped air | Tape not pressed firmly or wrapping completed too quickly | Apply controlled pressure during each wrapping pass |
| Uneven coating build | Inconsistent overlap or uncontrolled tape angle | Mark or monitor the wrapping path and overlap |
| Inner layer movement during outer wrapping | Excessive outer-wrap tension or insufficient inner-layer adhesion | Review primer condition and outer-wrap application tension |
| Poor transition to existing coating | Insufficient overlap or contaminated existing coating | Clean and prepare the transition area according to the approved procedure |
| Tape narrowing | Excessive stretching during application | Apply only the manufacturer-recommended tension |
Why a Representative Wrapping Trial Is Valuable
For a large project, a representative trial can identify installation problems before mass production or site application begins.
The trial should use:
- The proposed primer
- The proposed inner wrap tape
- The proposed outer wrap tape
- The actual or equivalent pipe diameter
- The specified bend radius
- The proposed tape width
- The required overlap
- Representative application temperature
- The proposed surface preparation method
The trial should evaluate:
- Tape conformability
- Wrinkle formation
- Edge lifting
- Continuity of overlap
- Adhesion between layers
- Start and finish details
- Completed coating appearance
- Material consumption
- Installation time
- Inspector acceptance
Where necessary, the results can be used to prepare a project-specific Application Procedure Specification or approved installation method.
Information Buyers Should Provide
To recommend a suitable cold-applied tape system for pipeline bends, the manufacturer requires more than a total product weight.
The following information should be provided wherever possible:
| Information Required | Why It Matters |
|---|---|
| Pipe outside diameter | Affects tape width, coverage and wrapping geometry |
| Bend angle | Determines the length and complexity of the coated area |
| Bend radius | Affects tape conformability and the risk of wrinkling |
| Number of bends | Required for quantity calculation |
| Existing pipe coating | Determines compatibility and transition requirements |
| New construction or rehabilitation | Influences surface condition and installation method |
| Buried, submerged or above-ground service | Affects mechanical and environmental requirements |
| Minimum application temperature | Influences primer drying and tape handling |
| Maximum operating temperature | Influences long-term system performance |
| Soil and environmental conditions | Helps assess mechanical and corrosion exposure |
| Required tape thickness | Defines the proposed tape construction |
| Preferred tape width and roll length | Affects installation and packaging |
| Required overlap | Affects completed thickness and material quantity |
| Surface preparation requirement | Influences adhesion and system qualification |
| Applicable standards | Defines test and acceptance requirements |
| Inspection requirements | Determines documentation and site quality control |
| Delivery destination | Supports packaging and logistics planning |
Providing this information at the enquiry stage reduces the risk of quoting an unsuitable configuration or incorrect quantity.
Technical Documents to Request
A professional technical submission for pipeline bend coating should normally identify the actual products proposed and may include:
- Technical Data Sheets for primer, inner tape and outer tape
- Safety Data Sheets
- Manufacturer’s compatibility statement
- Product construction and dimensional data
- Tape width and roll length
- Net weight per roll
- Primer coverage and drying information
- Application and operating temperature ranges
- Installation instructions
- Surface preparation requirements
- Recommended overlap
- Packaging information
- Certificate of Analysis or Certificate of Conformity
- Quality management certificates
- Relevant laboratory test reports
- Country-of-origin declaration
- Warranty conditions
- Preliminary material quantity calculation
Technical documents should clearly distinguish between tested values, declared nominal values and project-specific requirements.
Individual tape tests and complete coating-system qualification should not be treated as interchangeable. A property test may evaluate one characteristic of a tape, while a system test evaluates the combined performance of the primer, tape layers and prepared steel substrate.
When Conventional Wrapping Tape May Not Be the Best Choice
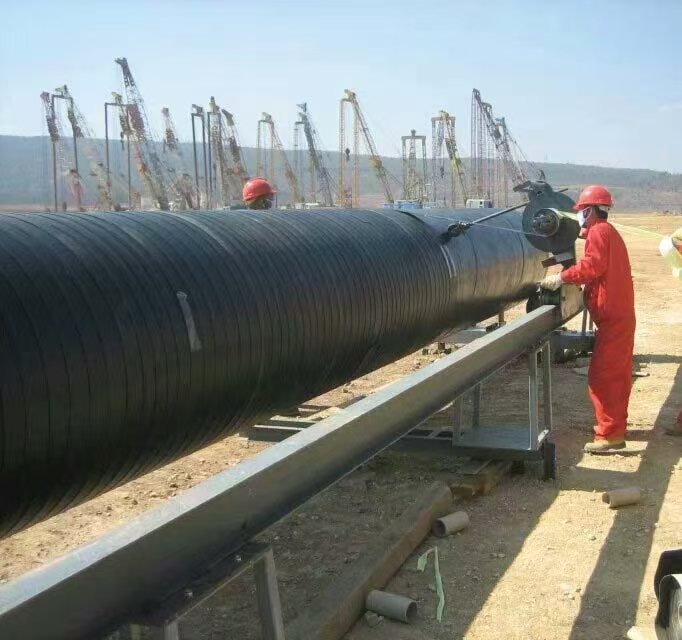
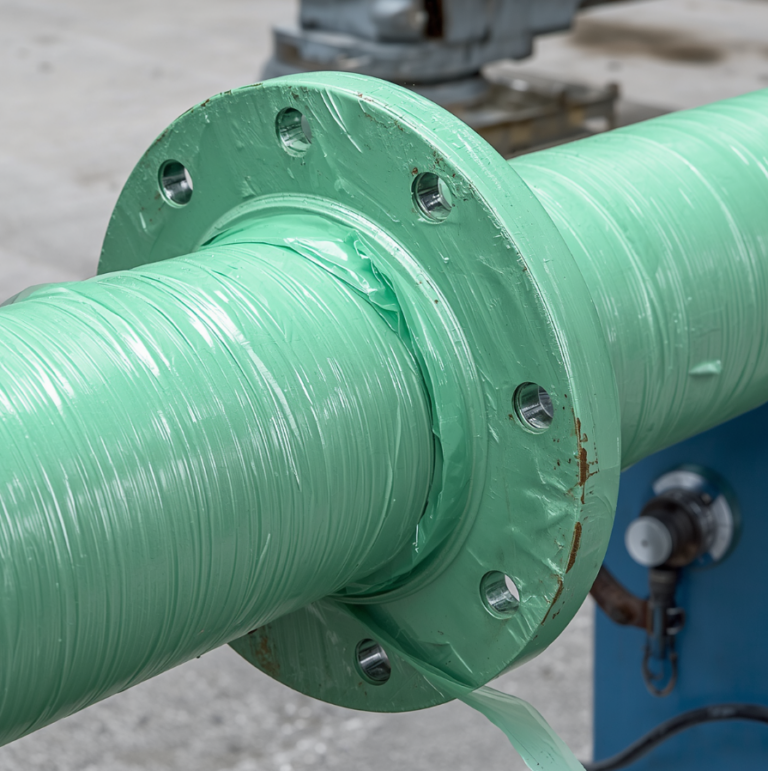
Cold-applied polyethylene tape is commonly used for regular pipe surfaces, bends, elbows, fittings and coating repair applications when the product and installation method are suitable.
However, highly irregular components may require a different corrosion protection approach.
Examples include:
- Flanges with deep bolt recesses
- Complex valves
- Pumps and connections
- Tees with difficult transitions
- Irregular fabricated fittings
- Components with multiple sharp changes in geometry
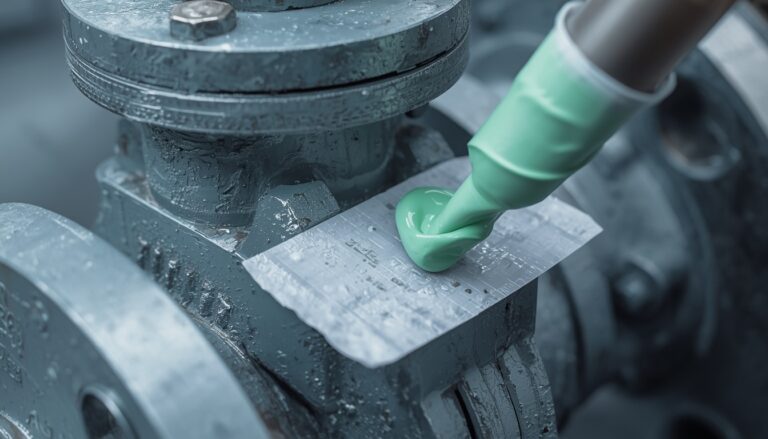
For these applications, a viscoelastic paste and tape system may provide better gap filling and conformability.
Similarly, pipeline field joints may use heat-shrinkable sleeves where required by the pipeline coating design and project specification.
The most effective approach is to select the appropriate protection system for each pipeline area rather than expecting one material to solve every corrosion problem.
How Jiayu Supports Pipeline Bend Coating Projects
Langfang Zhongyou Jiayu Anti-Corrosion Technology Co., Ltd. manufactures pipeline corrosion protection materials for new construction, maintenance and rehabilitation projects.
Jiayu can support technical and commercial discussions involving:
- Polyethylene anticorrosion adhesive tape
- Inner and outer wrap configurations
- Compatible pipeline primer
- Tape thickness selection
- Tape width and roll-size selection
- Pipeline bend and elbow applications
- Surface preparation and wrapping procedures
- Packaging and material quantity calculations
- Technical documentation
- Product samples
- Project-specific manufacturing requirements
Recommendations are made according to the pipe dimensions, bend geometry, service conditions, project specifications and technical information provided by the customer.
For product information, visit our Cold-Applied Tape range.
Technical installation documents are also available through the Jiayu Download Center.
Frequently Asked Questions
Can cold-applied tape be used on pipeline bends?
Yes, provided that the selected tape construction, width, flexibility and installation method are suitable for the pipe diameter and bend geometry. A representative wrapping trial may be advisable for critical or large-volume applications.
Is narrower tape always better for bends?
Not necessarily. Narrower tape may improve conformability on tight bends, but it also requires more wrapping passes and overlaps. The final selection should balance installation control, productivity, coating build and material consumption.
Can the same tape be used as both inner and outer wrap?
The products may belong to the same product series, but their construction and functions can be different. The technical documentation should clearly identify the backing thickness, adhesive thickness and intended use of each layer.
Is primer always required?
Primer is normally an essential component of a conventional polyethylene adhesive tape coating system. Any proposal to omit primer should be supported by the manufacturer’s written instructions and accepted by the project specification.
How much overlap should be used on a bend?
The overlap should follow the approved manufacturer’s instructions and project specification. It must remain consistent across both the inside and outside radii of the bend.
How is the required tape quantity calculated?
The calculation should consider pipe diameter, coated length, bend geometry, tape width, roll length, specified overlap, number of layers and installation losses. The final order quantity should also be rounded to the manufacturer’s standard packaging quantity.
Which information is needed before recommending a tape system?
At minimum, the manufacturer should receive the pipe outside diameter, bend angle, bend radius, application temperature, operating temperature, existing coating, service environment, required standard and preferred tape dimensions.
Conclusion
Pipeline bends and elbows require more careful material selection and installation control than straight pipe sections.
A reliable cold-applied coating system depends on the combined performance of the compatible primer, inner wrap tape and outer wrap tape. Tape width, flexibility, backing-to-adhesive construction, overlap, surface preparation, application tension and temperature conditions all influence the completed coating.
The correct product cannot be selected from nominal thickness alone.
For important projects, a representative bend-wrapping trial can help verify conformability, overlap, installation method and actual material consumption before full-scale application.
Need assistance selecting a cold-applied pipeline wrapping tape system for bends, elbows, fittings or repair areas?
Contact Jiayu’s technical and sales team and provide your pipe dimensions, bend geometry, operating conditions, applicable standards and delivery destination. We can assist with product configuration, technical documentation, packaging and preliminary material quantity calculations.